EN
 DE
 RU
 PT
 JA
 ES
 IT
FLAT WELDING BURR-FREE / POWDER COATING / ACCEPTANCE CHECK
A weld bead that catches a glove is a safety finding, not a finish complaint
EHS and 5S audits keep raising the same two issues on guarding: a protruding weld that cuts an inspector’s hand, and rust blooming out of a weld crevice a few months into a humid shift. Both start at the joint. Flat welding burr-free construction puts the wire flush with the tube and fully welds every contact point, so there is no sharp edge and no open pocket to hold moisture. An epoxy-polyester electrostatic powder coating tested to ISO 9227 neutral salt spray then protects the steel, within the limits of the service environment.
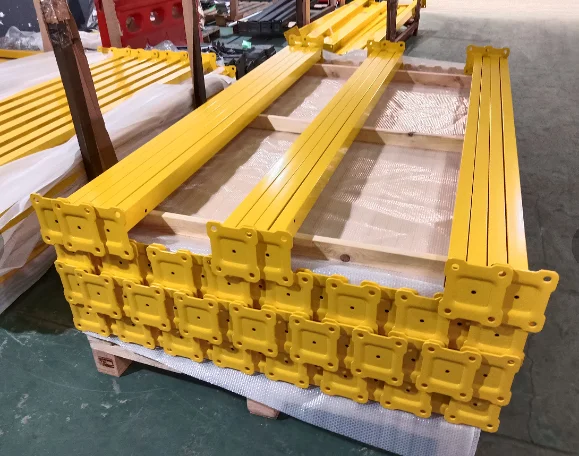
Why joint shape decides corrosion life
A proud, intermittent bead leaves a crevice at every wire crossing. Cleaning fluid and condensation sit in that crevice, the coating is thin at the sharp edge, and corrosion starts from the inside of the joint. A flat, fully welded joint has no pocket and no peak for the coating to pull away from.
| Detail | What the acceptance check looks for |
|---|---|
| Wire to frame joint | 3.0 or 4.0 mm wire welded flat into the 20x30x1.5 mm tube, wire not standing proud of the tube face. |
| All contact points | Fully welded, with no missed intersections or open laps. |
| Surface after grinding | Smooth to a gloved hand along the whole perimeter; no burr at panel ends or gate edges. |
| Coating | Epoxy-polyester electrostatic powder, continuous over welds and cut edges, no misses inside frame corners. |
| Evidence | ISO 9227 neutral salt spray test reference and GB/T 9286 adhesion reference in the handover file. |
Three checks at handover, and one honest limit
Check the weld with a glove, not a datasheet
Run a gloved hand along the frame, across the wire ends and around the gate latch edges. Flat welding burr-free means the wire is welded into the inner face of the tube and ground flush, so nothing catches. It is also a rigidity check: an intermittent bead may look clean in a photograph but will open under panel flex. Because every contact point is fully welded, the mesh and the 20x30x1.5 mm border behave as one section rather than a loose sheet held in a frame.
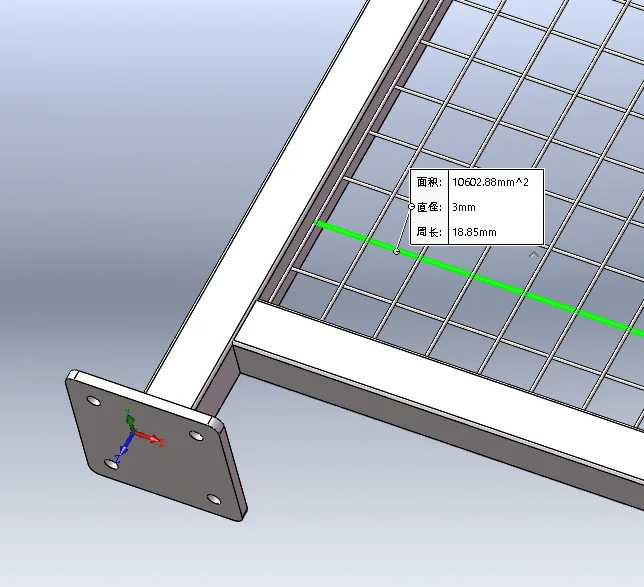
Look for missed coating where it is hardest to spray
Inspect the inside corners of the frame, the underside of the base plate and the weld toes. Those are the places a thin coat shows up first, and they are the places a humid or wash-down cell attacks. The epoxy-polyester electrostatic powder finish is applied after fabrication and is referenced in the product documentation together with ISO 9227 neutral salt spray testing and GB/T 9286 adhesion. Ask for the test reference on the actual batch, not a generic certificate copied from another project.
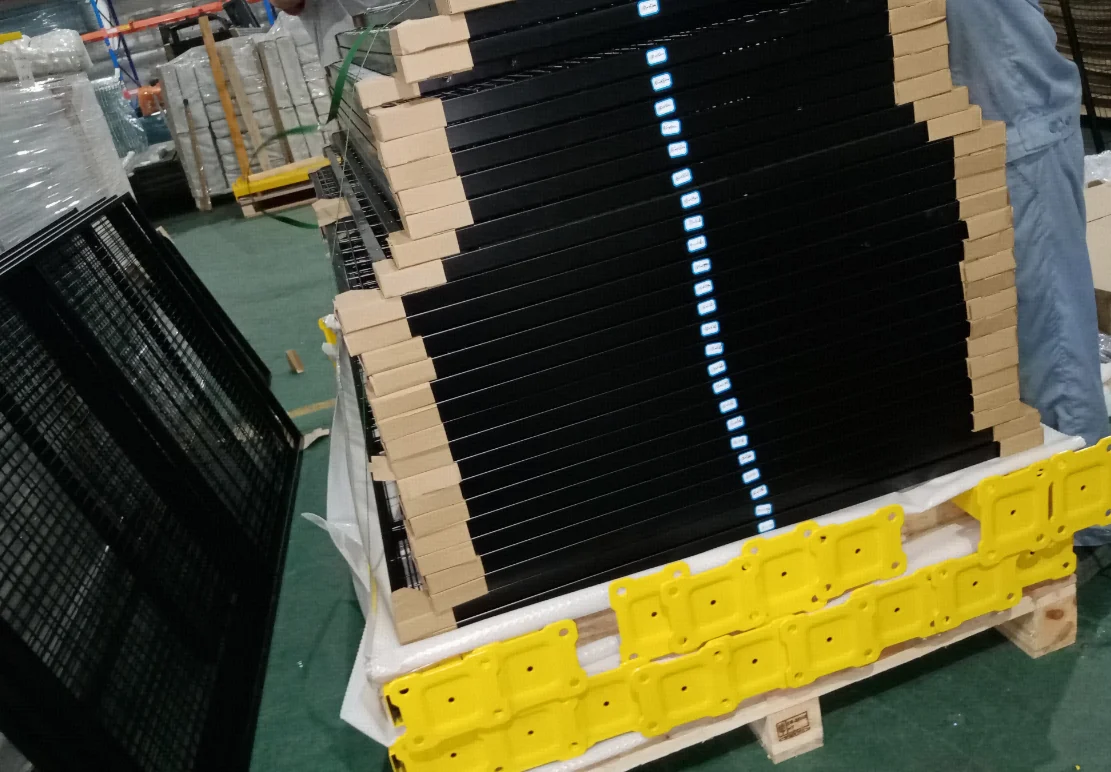
State what the coating does not promise
A salt spray test is a comparative laboratory result, not a service-life guarantee for every plant. Cutting fluid, alkaline cleaners, solvent wash-down and constant humidity will age any organic coating, and impact damage or a site-made weld breaks it locally. Treat the finish as a consumable layer: record the baseline at handover, add it to the inspection round, and touch up chips with the specified repair material. ISO 9227 salt spray powder coating evidence supports the specification at delivery; it does not remove the need for periodic inspection.
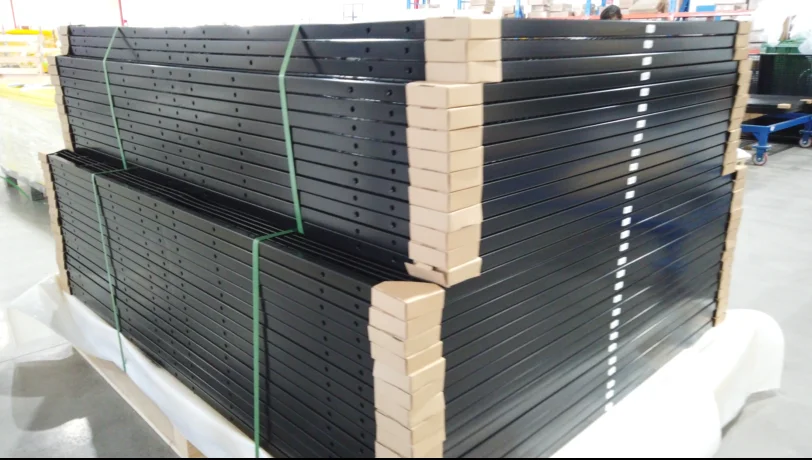
Plants where this detail gets checked twice
- Machining halls with high humidity and regular coolant mist.
- Food, beverage and wash-down areas using alkaline cleaning agents.
- 5S and EHS programmes that score hand-contact edges during safety walks.
- Export projects where the finish condition is recorded at container loading.
- Cells planned for relocation, where panels are handled and re-clamped repeatedly.
In each case the acceptance record should name the flat welding burr-free requirement, the coating system and the inspection interval. That turns a visual complaint into a checkable item.
What to put in the acceptance sheet
Include the weld appearance requirement, a gloved-hand check, a coating coverage check at frame corners, the ISO 9227 test reference for the batch, and the agreed repair procedure for chips. Add the cleaning agents used on the line so the maintenance interval reflects the real environment.
Get the finish requirement written into the order
Tell us the cleaning regime and the humidity in the cell. We will return the weld and coating acceptance checklist with the inspection interval that matches your environment.