EN
 DE
 RU
 PT
 JA
 ES
 IT
WELDING SPARK GUARD PANELS / CNC MACHINE GUARDS / PANEL INFILL
One mesh aperture cannot answer for chips, arc flash and coolant at the same time
Fabricators running cutting and welding beside CNC machining often end up with home-made sheets of plywood or acrylic cable-tied to the fence. They stop one hazard and create two more: blocked sightlines, trapped heat and a panel that nobody can inspect. Panel selection is a three-factor decision. Chip size sets the aperture and wire diameter; arc brightness sets the tint and whether an infill is needed; coolant and cleaning agents set the material. Welding spark guard panels and CNC machine guards are not one product but a module choice made on the same frame.

Three factors, in the order they should be checked
Fine chips decide the aperture. Arc decides the optical density and colour. Liquid decides the panel material and the sealing detail. Checking them together avoids the common mistake of fitting a transparent sheet that survives the sparks but clouds over under coolant.
| Factor | Panel response |
|---|---|
| Fine metal chips and gypsum dust | 20×100 mm mesh with 3.0 or 4.0 mm wire stops the coarse fraction; add a closed infill where fine dust must not pass. |
| Welding arc and flash | Transparent, bronze or red plastic panels reduce flash at adjacent stations; choose by the welding process, not by colour preference. |
| Coolant, cutting fluid and wash-down | Solid metal sheet or a plastic infill rated for the cleaning agent; check the 60 °C limit and the UL94 V0 and EN 1598 listing. |
| Heat and hot spatter | Steel sheet rather than plastic where spatter can land on the surface. |
| Visibility and ventilation | Closed panels reduce both; position them only on the affected bays and keep mesh elsewhere. |
How the infill stays a module, not a site modification
Narrow mesh first, then decide what still gets through
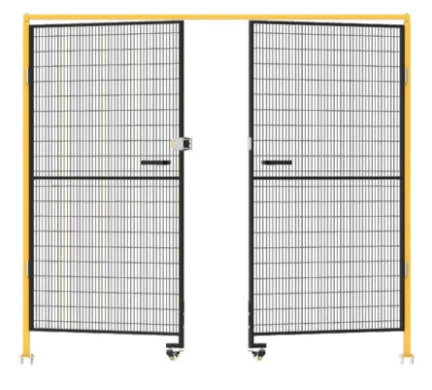
A framed panel with a 20×100 mm aperture and 4.0 mm wire, welded flat into a 20x30x1.5 mm tube border, removes most flying swarf before any add-on is considered. That matters because a closed sheet over the whole run costs sightlines, airflow and cleaning access. Zone the run: keep open mesh on inspection sides, put closed infill opposite the spindle or the arc, and record the zone on the layout drawing so the panel schedule is auditable.
Tint is a process choice
Transparent, bronze and red plastic panels are listed in the product documentation for reducing welding flash. They are not interchangeable: a bronze panel that suits a manual welding bay can make a machining centre hard to inspect, and a red one changes how operators read indicator lights. Transparent polycarbonate keeps the process visible where the arc is intermittent. All three options are also bound by the same 60 °C heat limit and the UL94 V0 and EN 1598 fire listing, so a hot-spatter zone still needs steel.

Fix the panel to the frame, not to the floor
Plastic and metal infills are supplied as covered mesh modules that use the same clamp rings and M8 fixings as the standard panel. That is the point: a tinted or solid bay can be swapped in a maintenance window without cutting, drilling or adhesive. Site-glued sheets have no retention case, no documented fire rating and no place in a handover file. Fully closed bays also change airflow around the machine and can trap heat or mist, which is another reason to limit them to the bays the risk assessment names.

Typical zone-by-zone selections
- CNC machining centres with fine aluminium chips and high-pressure coolant.
- Prefabricated board and gypsum cutting lines producing light airborne dust.
- Robotic and manual welding bays sharing an aisle with assembly operators.
- Grinding stations where hot particles reach the neighbouring workstation.
- Mixed cells where inspection windows must stay clear while the process side is closed.
In each layout the panel choice follows the process list. Welding spark guard panels go where arc and spatter are present; CNC machine guards on the machining side keep the narrow mesh where visibility and airflow still matter.
What to specify in the panel schedule
List each bay, the hazard present, the panel type, the tint, the fixing kit and the cleaning agents used on the line. Include the 60 °C limit and the UL94 V0 and EN 1598 reference for any plastic infill so the acceptance reviewer can see the boundary of the rating.
Send the process list, not a photo of the fence
Tell us which cutting, welding and washing operations sit behind each bay, and we will return a panel schedule with mesh, tinted infill and solid sheet assigned to the zones that need them.