ES
 EN
 DE
 RU
 PT
 JA
 IT

1.Raw material procurement
The main raw materials to be purchased for this product are 50*50mm galvanized square pipe and 2mm diameter wire roll.
2.Pipe Cutting
 (1) Place the pipe to be cut on the laser cutting machine and keep it horizontal and stable.
(2) According to the diameter of the pipe, material, thickness and other parameters, set the cutting parameters of the laser cutting machine, including laser power, cutting speed, focal length and other parameters.
3) Debug the laser cutting machine so that it can cut the pipe accurately, adjust the height and position of the laser head to ensure that the laser beam accurately irradiates the surface of the pipe.

4) Start the laser cutting machine so that it begins to cut the pipe. In the cutting process, you need to observe the cutting situation in time to ensure the cutting quality and cutting speed.
5) After the cutting is completed, remove the pipe from the laser cutting machine, clean up the scene and do a good job of maintaining the equipment.
3. Wire cutting, welding
(1) First of all, put the whole bundle of wire into a disk that can be rotated, and put one end of the wire into the hole of the straightening machine. The wire passes through the upper and lower two rollers, which exert pressure on the wire to straighten the bent wire.
(2) After passing through the straightening machine, the wire will be cut and fall according to the set distance to bundle a certain number of wires. The bundled wire is sent to another production line with a hanging machine.
3) At this time in another section of the production line, dozens of wire coils are running at a constant speed, and these wires pass through the straightening machine at the same time, while the other end of the machine drops the previously cut wires into the conveyor, which drops the wires according to a certain interval, and welds them at the same time as they come into contact with the wires.
4) The welded wire mesh is quickly transferred to the cutting table, and the whole process of cutting is automated without manual operation. After cutting, a whole sheet of wire mesh is transferred to a forklift truck, which transports the wire mesh to the overall welding workshop after turning full.
4. Integral Welding


1)Weld the outer frame of the square tube, don’t weld too close to cause deformation of the frame when welding.
2) Weld the mesh to the outer frame.

5.Grinding and chamfering
Grind, chamfer and deburr the welded mesh.
6.Plastic spraying
1) Shot blasting. After grinding the whole guardrail and columns for shot blasting treatment, with electro-mechanical shot blasting machine as the driving force, the use of shot blasting machine thrown high-speed projectiles to clean up or strengthen the surface of the metal workpiece, and increase the surface of the guardrail adsorption capacity of plastic powder. The principle of shot blasting and sand blasting is different, sand blasting is the use of air highly compressed for processing, while shot blasting is through the impeller turned out to tell the projectile processing
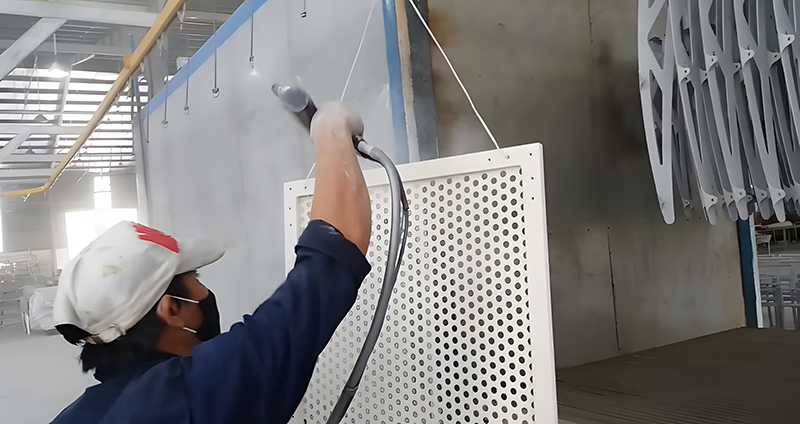
2) Plastic powder spraying. After sandblasting the mesh and columns for powder spraying, powder spraying should pay attention to the surface spraying complete, uniform thickness.
(3) heating curing. Plastic spraying mesh and columns into the curing furnace, heated to a predetermined temperature (generally 185 degrees), and keep warm for a corresponding period of time (15 minutes), open the furnace will be taken out of the finished product.
7.Quality Inspection
Inspect the shape, size, surface quality and welding quality of the products.
Interlock Switch Mounting Without Drilling: Why Alfence T-Slot Posts End Phantom Stops
Bolting an interlock switch bracket through a powder-coated steel post drills the coating, drops swarf into the cell and leaves a rust line — and when the hinged leaf sags, the tongue misaligns and the PLC reports a phantom guard fault. Alfence mounts sensors, e-stops and conduit in the T-slot groove of a 40×40 mm or 45×45 mm aluminum post, with door hardware sized to keep the safety switch aligned.
Phantom Safe Torque Off Stops: T-Slot Guarding Fence Posts Mount Interlocks Without Drilling
Painted steel guarding posts force maintenance to drill for interlock switches, dropping swarf in the cell and breaking the coating where rust starts. Sagging hinge doors then misalign the interlock tongue and the PLC trips Safe Torque Off while the gate is closed. Alfence industrial safety fence mounts sensors, e-stops and cable routing into the T-slot aluminum profile post without drilling, and uses hinged, folding or sliding door frames that keep interlock geometry stable - protecting OEE through phantom stops and line changes.
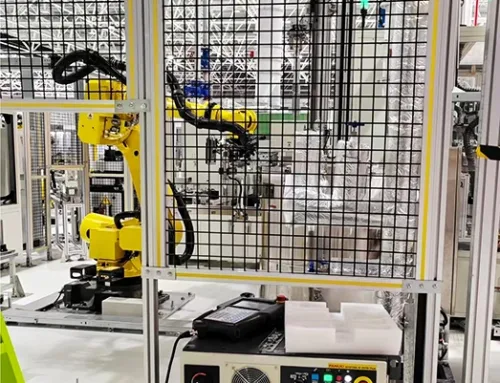
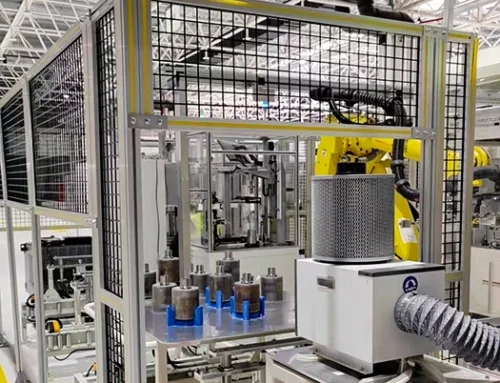
Automotive Plant Industrial Safety Fence: Keep the Robot Cell Close to the Hazard
Automotive plants cannot afford to lose production floor to an oversized machine guarding perimeter. Alfence combines 20×100 mm mesh with slim 40×40 mm or 45×45 mm aluminum posts for a compact, reconfigurable industrial safety fence layout, with final clearance confirmed by the project risk assessment.